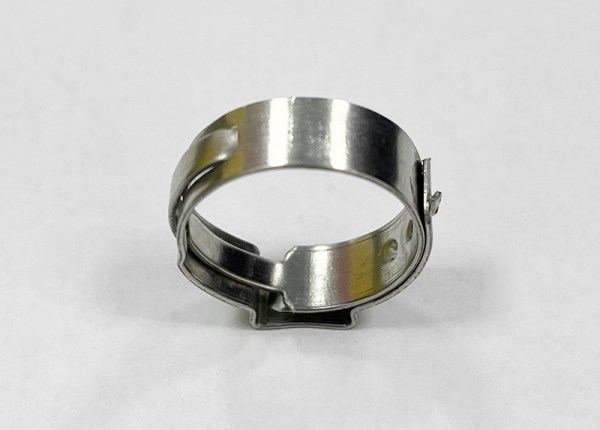
Hardware shrapnel clips with bright tin can enhance cathodic polarization and dispersion capabilities, making the coating’s crystallization delicate and shiny, while also masking metal impurities. Inorganic brighteners include nickel sulfate or ammonium salt. This can give the clips better weldability and corrosion resistance. However, if discoloration occurs after plating with bright tin, how can we solve this issue?
If discoloration occurs after hardware shrapnel clips with bright tin, we can remove the film using a 10% phosphoric acid solution before the clips dry after tinning, and then wash several times with hot and cold water.
Plated tin clips should not be washed with anti-current flow, as this will lead to water fogging on the tin surface. We can first pour the clips into a basin, immediately pour in clean water to stir, then pour out the water, repeating this three times. After that, the clips should be soaked in a diluted sodium phosphate solution at about 50°C for three times, followed by cleaning, and pre-plating on a copper substrate.
Neutralization and passivation should be carried out after electroplating to neutralize residual acid and form a protective film on the tin surface. During electroplating, the plating metal or other insoluble materials act as the anode, while the clips to be plated serve as the cathode, where the cations of the plating metal are reduced on the surface of the workpiece being plated to form a coating. To eliminate the interference of other cations, and to ensure a uniform and firm coating, a plating solution containing cations of the plating metal should be used to maintain a constant concentration of the cations in the plating solution. Neutralizers generally use weakly alkaline phosphates. After neutralization, it is washed into the passivation process. The passivation solution at 60-80°C is a chromic salt solution, which passivates for 2 minutes, forming a layer of oxide on the tin surface.
To prevent the tin coating from turning yellow, attention must be paid to poor washing after electroplating, excessive current density, and temperature of the plating solution. The coating has effectively been passivated against discoloration, but it must be thoroughly cleaned, and a solution of saturated stearic acid should be used to form a protective film on the surface of the hardware shrapnel clips.